Description
Understanding the Servo Vacuum Hot Press Cooling Press by Taihe Machinery
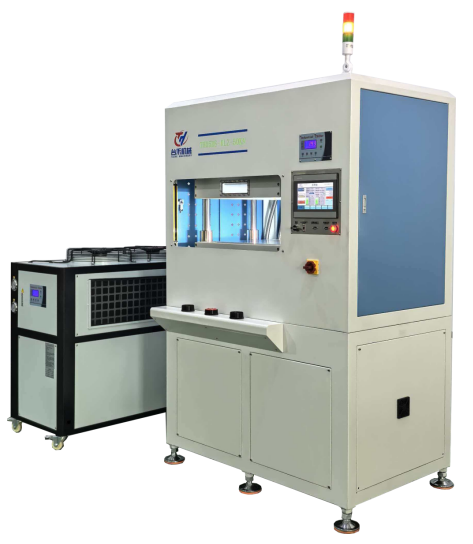
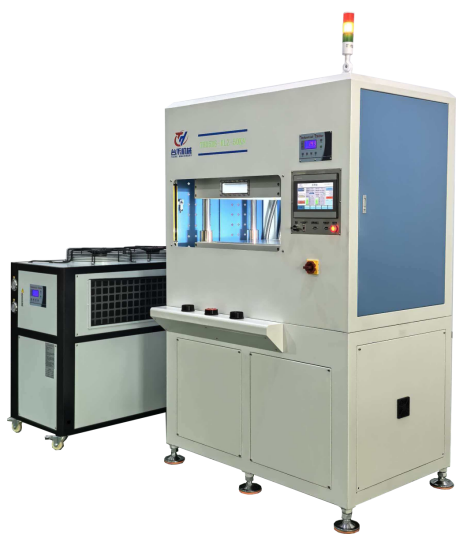
For manufacturers working with multi-layer ultra-thin composite materials, the process of bonding layers without introducing bubbles, internal stress, or surface damage remains a persistent engineering challenge. Taihe Machinery addresses this with its Servo Vacuum Hot Press Cooling Press, a piece of precision lamination equipment built around a single operating philosophy: vacuum degassing plus constant-temperature hot pressing plus pressurized water-cooled shaping. This combination is designed specifically for the precise lamination of multi-layer ultra-thin composite materials, including MEA membrane electrode assemblies, flexible printed circuits (FPC), and carbon fiber film materials.
Technical Capabilities That Define Process Control
At the core of the system is an integrated technology platform that brings together a servo pressure drive, a vacuum sealed chamber, a flat panel heating system, a water-cooled cooling system, and a data acquisition control system. Rather than treating these as separate modules, Taihe Machinery has unified them so that pressure, temperature, and displacement can be managed in real time throughout the entire pressing cycle.
Several technical metrics underpin this control:
- Vacuum degree is process-configurable, allowing operators to match evacuation levels to specific material requirements.
- Servo descent speed is segment-adjustable, enabling a smooth, staged approach rather than a single uniform motion.
- Temperature is maintained through PID control, holding the plate surface at a consistent set point.
- Pressure is maintained through real-time sensor feedback and dynamic compensation, correcting for fluctuations as they occur.
- Cooling rate is adjustable, giving operators flexibility based on the material being processed.
Data Capabilities and Traceability
Beyond the mechanical and thermal systems, the press is built to generate usable process data. It continuously collects pressure, displacement, and temperature data throughout each cycle, automatically generating pressure-displacement and temperature-time curves. Every process record is saved automatically, removing the need for manual logging.
This data does not remain locked inside the machine. The system supports USB drive export or MES system integration, giving manufacturers a path to incorporate production data into broader quality systems. This openness to traceability means that when a batch needs to be reviewed, the underlying pressure and temperature history is already documented and accessible.
Addressing Key Pain Points in Multi-Layer Lamination
The design choices behind the Servo Vacuum Hot Press Cooling Press map directly to recurring problems in ultra-thin composite lamination:
- Trapped air between layers can cause bubbles or voids after lamination. The system’s vacuum evacuation step removes air enclosed between material layers before pressing begins.
- Cooling shrinkage after heating can create internal stress, leading to springback, warpage, delamination, and blistering. The pressurized water-cooled shaping stage keeps pressure applied while the material cools, offsetting this shrinkage stress.
- Improper pressing contact can scratch or misalign ultra-thin films. The servo closed-loop pre-pressing stage provides segment-adjustable, low-speed soft contact to reduce this risk.
- Lack of process data can make production quality difficult to trace. The integrated data recording and export functions address this directly.
Key Features Across the Full Production Cycle
Workpiece Placement and Chamber Closure
Pre-laminated workpieces—such as MEA membrane electrode assemblies, FPC, and carbon fiber film materials—are placed between upper and lower heated platens. Closing the chamber forms a sealed space, and high-precision pressure sensors and temperature probes transmit signals to the control system in real time.
Vacuum Evacuation
The cavity vacuum pump extracts air enclosed in the gaps between multi-layer materials, eliminating bubble and void risks after lamination. Vacuum degree is set according to the material process and maintained once evacuation is complete.
Servo-Driven Descent and Pre-Pressing
A servo motor drives a ball screw through a synchronous belt to lower the upper platen smoothly. Closed-loop control enables segment-adjustable descent speed and low-speed soft contact, protecting ultra-thin film materials. A small pre-pressure flattens and fixes the stacked layers to prevent slippage and misalignment.
Constant-Temperature Dwell
Heating rods built into the platens raise the temperature, while real-time feedback and PID control hold the plate surface at the set process temperature. Servo pressure output, combined with real-time sensor feedback and dynamic compensation, maintains constant pressure. Heat and pressure together soften and melt the polymer resin or ionomer, allowing multi-layer interfaces to bond. Dwell time is automatically timed according to the process recipe.
Pressurized Water Cooling and Shaping
After the dwell period, pressure remains unchanged—there is no pressure release or mold lifting. Heating stops, and the water-cooling circuit inside the platens circulates cooling water for uniform cooling. The material solidifies gradually under pressure, offsetting cooling shrinkage stress and preventing springback, warpage, delamination, and blistering. The cooling rate is controllable and adjustable to match material requirements, effectively turning this phase into a controlled, pressure-assisted shaping step as the laminate transitions from a heated to a cooled state.
Cooling Completion, Pressure Release, Mold Opening, and Discharge
When the platen temperature reaches the preset discharge temperature, the servo system releases pressure, the upper platen rises, the vacuum chamber breaks vacuum, and the formed workpiece is removed.
Whole-Process Data Recording
Throughout the cycle, the system continuously collects pressure, displacement, and temperature data, automatically generating pressure-displacement and temperature-time curves. Process records are saved automatically, with support for USB drive export or MES system integration for production data traceability.
Technical Highlights at a Glance
- Integrated servo pressure drive, vacuum sealed chamber, flat panel heating system, water-cooled cooling system, and data acquisition control system working as one platform.
- Closed-loop servo control for segment-adjustable descent speed and dynamic pressure compensation.
- PID temperature control with real-time temperature feedback.
- Water-cooled circuit that supports uniform cooling while pressure is maintained.
- Automatic process curve generation and record saving for traceability purposes.
Industry Adaptation and Delivery Model
The Servo Vacuum Hot Press Cooling Press is delivered as a physical industrial pressing machine with embedded control and data acquisition, supporting USB drive export or MES system integration out of the box. Its process focus centers on multi-layer ultra-thin composite material precision lamination, with demonstrated workpiece compatibility across MEA membrane electrode assemblies, flexible printed circuits, and carbon fiber film materials.
For manufacturers evaluating equipment where vacuum degassing, constant-temperature bonding, and pressure-maintained cooling all need to happen within a single, data-traceable cycle, Taihe Machinery’s Servo Vacuum Hot Press Cooling Press offers a structured approach: each phase of the cycle—from chamber closure through servo-driven pre-pressing, constant-temperature dwell, pressurized water cooling, and final discharge—is built to directly counter the specific pain points of bubbling, internal stress, film misalignment, and data loss that are common in ultra-thin composite lamination work.


Reviews
There are no reviews yet.